Moisture content specs for teak: 8% vs 12%
What moisture content actually controls
Moisture content is the single most useful predictor of how a teak component will behave after it leaves the factory. It controls dimensional movement, glue-line integrity and surface finish, and it determines whether a frame that fits on the assembly floor still fits after a month in a warehouse. A 600 mm wide teak slat can move roughly 3 to 4 mm across the grain for every 4% change in moisture content, which is enough to open a miter joint or crack a finish.
The movement is not uniform. Tangential shrinkage in teak is roughly 5% to 6% from green to oven-dry, radial shrinkage roughly 2.5% to 3.5%, and the volumetric figure is around 7% to 9%. Wood moves least along the grain and most tangentially, which is why a tabletop glued up from flatsawn strips can cup while a quarter-sawn top of the same species stays flat. Moisture specification is therefore inseparable from grain orientation.
Glue lines are the second constraint. Polyurethane and PVAc adhesives used in outdoor furniture have a working moisture window, generally around 6% to 12% for the substrate. Below that range the wood starves the glue of the moisture it needs to cure; above it the glue foams, the joint creeps and the bond line fails under cyclic humidity. Surface finish has a similar sensitivity: a board dried to 6% that absorbs humidity before coating will raise grain and show sanding marks through the film.
Why 8% and 12% are both defensible
An 8% target suits dry or conditioned markets: northern Europe, inland North America, Japan in winter, and any product that will spend its life in air-conditioned interiors. In those environments the equilibrium moisture content of wood sits near 6% to 9% for much of the year, so a product shipped at 8% arrives close to its service condition and moves very little. The trade-off is that 8% wood is more expensive to produce and more vulnerable to rapid moisture uptake in transit.
A 12% target suits humid and coastal markets: the Gulf states, Southeast Asia, the Mediterranean coast, the southern United States and any unheated outdoor setting. There the equilibrium moisture content is frequently 12% to 16%, so a board shipped at 8% will swell on arrival, sometimes enough to bind a drawer or split a glued panel. Shipping at 12% means the product arrives near equilibrium and simply does not move.
The mistake is to treat one number as universally correct. The specification should be derived from the destination market and the product exposure class, and it should be stated as a range with a gradient limit rather than a single figure. For a product sold across multiple climate zones, a mid-range target of 10% with a documented gradient limit is often a better commercial compromise than forcing either extreme.
Kiln schedules for plantation teak and the shell-to-core gradient
Plantation teak from Indonesia, Costa Rica or Brazil typically arrives at 40% to 80% moisture content and needs a controlled drying schedule rather than a fast kiln cycle. A practical schedule starts with a low initial dry-bulb temperature, around 40 C to 45 C, with a wet-bulb depression of 2 C to 4 C, and increases the depression stepwise as the moisture content falls. The final equalizing and conditioning stage runs at a small reversed gradient to relieve case-hardening.
Schedules are usually written to a reference thickness, and thicker stock dries more slowly. The drying gradient between the shell and the core is the variable that causes most field failures: a board that reads 10% on the surface but 16% at the center will continue to shrink internally after machining, producing internal checking, warp and joint separation. A common acceptance limit is a shell-to-core gradient of 2% or less, measured on freshly cut sections from a sample of boards.
Case-hardening is the related defect. The outer fibers dry and set while the core is still wet, and when the board is resawn the stresses release and the board cups or splits. The remedy is a conditioning stage at the end of the schedule, not a longer drying time at the same temperature. A moisture-content check alone will not reveal case-hardening; a resawn sample and a stress test will.
Measuring properly: pin-type versus capacitance meters
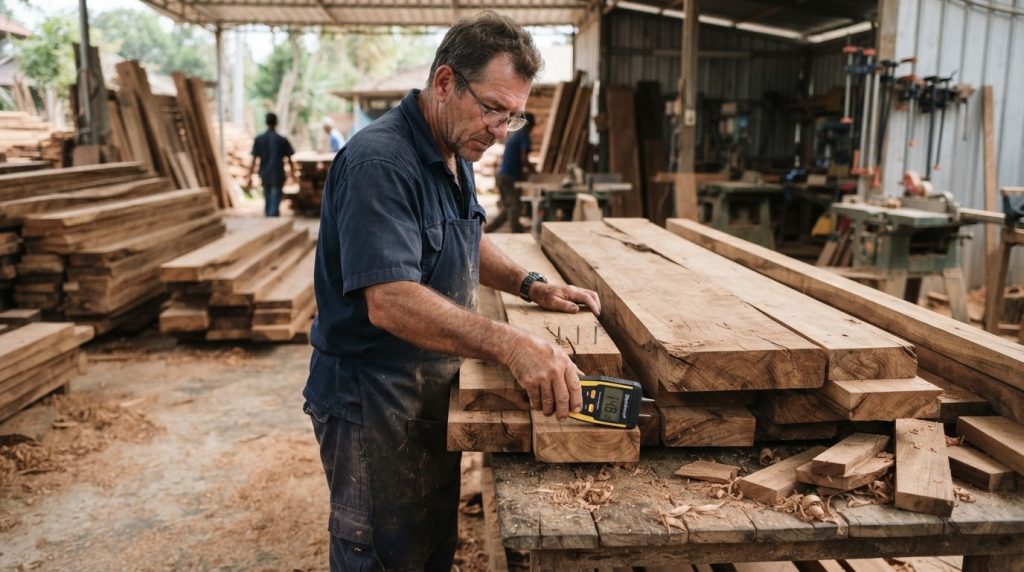
Pin-type resistance meters are accurate but destructive, because the reading depends on the depth of the pins. For a 25 mm board, insulated pins that read at the core are needed; standard uninsulated pins read an average that is biased toward the wetter surface layer. Pin meters also depend on species corrections: teak is more resistive than the reference species used to calibrate most meters, so a raw reading must be adjusted or the meter must be set to the correct species group.
Capacitance meters are non-destructive and fast, which makes them suitable for 100% screening on the production line, but they read a shallow field, typically the outer 20 to 25 mm, and they are sensitive to density, surface moisture and metal in the frame. The practical protocol is screening with capacitance and verification with pins.
Sampling size matters more than meter brand. A workable rule for a production lot is to sample at least 10% of boards, with a minimum of 20 pieces, drawn across the thickness range and the drying batch. The specification should name the meter type, the probe depth, the species correction, the sample size and the acceptance test, so that the buyer and the supplier are measuring the same thing.
Container humidity and equalizing before packing
A container moving from a humid port through tropical waters and into a dry destination can cycle through a wide humidity range over 30 days. Without protection, condensation forms on the underside of the container roof and drips onto the cargo, and wood that was at 12% can absorb enough moisture to reach 16% or more. Container rain is a recognized cause of mold, rust on hardware and swollen joints.
The two controls that matter are desiccant and equalization. Desiccant bags sized to the container volume and the voyage length absorb the moisture that enters through the door gaskets, and they must be positioned to allow airflow rather than packed flat against the cargo. Equalization means holding the finished product in the packing area long enough for the moisture to redistribute to a stable average before the cartons are closed, typically 24 to 72 hours depending on thickness and the difference between the yard and the packing area climate.
Wrapping is the third control. Stretch film that seals the whole pallet traps moisture and creates a microclimate; vented wrapping or breathable covers allow the product to equalize rather than sweat. For high-value products, a data logger placed inside a representative carton provides an actual record of the voyage conditions, which is far more useful in a dispute than an assumption about what the container experienced.
What to put in the specification
A complete moisture specification states the target range in percent, the gradient limit, the meter type and probe depth, the species correction, the sample size and the acceptance test. A typical line might read: moisture content 10% to 12% as measured by insulated-pin resistance meter at core depth on a 10% sample with a minimum of 20 pieces, shell-to-core gradient not exceeding 2%, no visible case-hardening on resawn samples.
The specification should also state when the measurement is taken. A reading taken at the drying kiln is not the same as a reading taken at the packing line, and a reading taken at the packing line is not the same as what the container will deliver. For products that will be installed in a different climate, the target should be set to the destination equilibrium moisture content, not to the factory ambient conditions.
Finally, a moisture specification is only as good as the record behind it. Each drying batch should have a batch number, a schedule record, the moisture readings and the samples that were cut for gradient checks. When a joint opens six months after installation, that record is what allows the factory and the buyer to determine whether the wood was out of specification or whether the installation environment was outside the agreed service class.